 EN

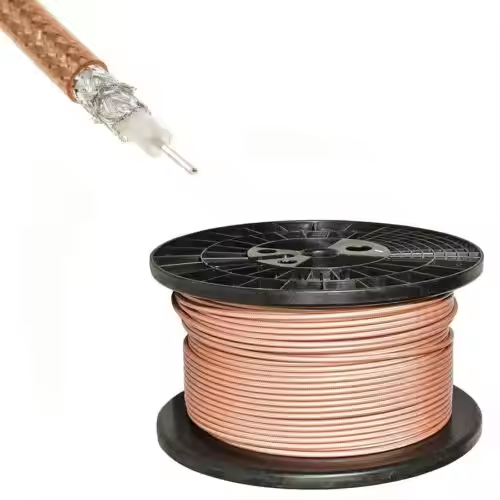
For RF engineering teams and commercial procurement specialists, choosing a specialized rg cable factory goes beyond selecting standard part numbers from an online catalog. Establishing a reliable original equipment manufacturer (OEM) production process requires strict control over raw material procurement, mechanical tolerance limits, phase-matching capabilities, and factory quality assurance gates. Whether an OEM project requires flexible assembly utilizing precision rg 58 coax connectors, double-shielded high-temperature rg 142 coax jumpers, or miniature low-loss assemblies governed by rigorous rg 316 specs, a professional rg cable factory must execute a controlled engineering review long before mass manufacturing begins.
Relying on generic designations alone often leads to communication gaps between buyers and suppliers. An experienced rg cable factory acts as a technical partner, translating high-level application demands into detailed, highly repeatable manufacturing documentation.
Step-by-Step OEM Order Execution Workflow
To ensure smooth production transitions and avoid unexpected field failures, a qualified rg cable factory follows a structured five-stage OEM order execution lifecycle:
-
RFQ & Engineering Package Audit: The rg cable factory evaluates your initial Request for Quotation (RFQ) package against internal manufacturing limits. Engineers check interface compatibility, connector tooling availability, cable stripping machine tolerances, and automated testing setups. Any electrical or dimensional ambiguity is resolved during this review stage.
-
DFM Review & Commercial Alignment: The engineering team performs a Design for Manufacturability (DFM) review to optimize unit costs, define Minimum Order Quantities (MOQ), align pilot lot lead times, and freeze the formal Engineering Drawing Revision referenced on the purchase order.
-
First-Article Inspection (FAI) & Prototyping: Before launching serial production, the rg cable factory produces sample assemblies. These samples undergo comprehensive first-article inspection—including physical dimension verification, mechanical pull-force testing, crimp cross-sectioning, and complete vector network analyzer (VNA) sweep testing for VSWR and insertion loss.
-
Controlled Serial Manufacturing: Upon formal first-article sign-off, the rg cable factory locks the bill of materials (BOM) and assembly work instructions. Strict change-control protocols ensure no substitutions of raw coaxial cable, plating materials, or crimp ferrules occur without explicit written buyer authorization.
-
Final Quality Acceptance & Dispatch: Every completed shipment undergoes 100% automated continuity and pin-to-pin short testing, along with statistical sampling for RF sweep performance, PIM level compliance, and outer jacket insulation resistance. Shipments are released accompanied by complete inspection test records and raw material lot traceability logs.
Key Technical Comparison: Industrial RG Coaxial Cable Standards
Selecting the correct coaxial cable family requires evaluating conductor geometry, dielectric construction, operating thermal limits, and RF shielding efficiency. The comparison table below highlights critical parameters evaluated when placing custom production orders with an rg cable factory:
| Performance Parameter | Flexible Standard Coax | High-Temperature Double Shield | Miniature High-Flex Coax |
| Coaxial Reference | rg 58 coax connectors compatibility | rg 142 coax assembly | rg 316 specs compliant |
| Impedance / Shielding | 50 Ohm / Single Braid (~85%) | 50 Ohm / Double Silver Braid (>95%) | 50 Ohm / Single Silver Braid (>95%) |
| Center Conductor Type | Solid or Stranded Tinned Copper | Solid Silver-Plated Copper Clad Steel | Stranded Silver-Plated Copper |
| Dielectric Material | Solid Polyethylene (PE) | Solid PTFE (Fluorinated Ethylene) | Solid PTFE (Fluorinated Ethylene) |
| Jacket Temperature Limit | -40°C to +85°C (PVC) | -55°C to +200°C (FEP) | -55°C to +200°C (FEP) |
| Typical Target Frequency | DC to 1.0 GHz | DC to 8.0 GHz | DC to 3.0 GHz |
| Common Applications | Commercial Radios, Test Leads | Military Avionics, Radar, High-Temp RF | Dense Equipment Bays, Medical, DAS |
When designing assemblies around standard rg 58 coax connectors, the rg cable factory must verify center conductor crimp barrel dimensions and jacket wall thickness tolerances to prevent pull-out under field strain. For heavy-duty military and aerospace applications calling for rg 142 coax, factory technicians must apply controlled heating during boot shrink processes to protect the high-temperature FEP outer jacket from thermal stress. Meanwhile, builds governed by miniature rg 316 specs demand micro-precision stripping equipment at the rg cable factory to avoid damaging delicate silver-plated inner strands during connector termination.
Establishing an RF Specification & Quality Acceptance Plan
A professional rg cable factory enforces clear quality control checks at every stage of assembly. When finalizing your OEM purchasing documentation, incorporate these explicit criteria into your factory quality agreement:
-
Electrical Acceptance Verification: Require 100% factory screening for basic DC continuity and pin-to-pin shorts. For high-frequency RF links, define upper frequency sweep limits, maximum allowable insertion loss (in dB/meter), and peak VSWR targets (e.g., VSWR < 1.15:1 up to 3 GHz).
-
Mechanical & Interface Validation: Specify precision connector interface standards (such as SMA, BNC, N-Type, or TNC) fitted with gold-plated or silver-plated center contacts. Require the rg cable factory to perform contact retention testing and mechanical crimp pull-test checks against MIL-STD-202 specifications.
-
Environmental & Compliance Standards: Ensure your rg cable factory provides full material traceability certificates confirming compliance with international directives, including RoHS, REACH, and UL flame-retardancy standards (e.g., VW-1 or IEC 60332). For specialized military-grade builds, confirm that factory production processes align with MIL-DTL-17 requirements.
Procurement teams sourcing reliable custom pre-terminated assemblies can rely on established manufacturing references like
OEM Sourcing Checklist for Procurement Teams
Before approving purchase orders with an rg cable factory, run through this essential OEM procurement checklist:
-
Is the correct assembly drawing revision explicitly referenced on the order?
-
Have all technical requirements for rg 58 coax connectors, double-shielded rg 142 coax, or micro-scale rg 316 specs been translated into measurable test limits?
-
Does the rg cable factory quote break down lead time into drawing review, material stocking, first-article sample build, buyer sign-off, and mass production dispatch?
-
Have minimum order quantities (MOQs), pilot lot price breaks, customized labeling formats, and packaging requirements been frozen in writing?
-
Will the rg cable factory supply lot traceability data and signed inspection certificates inside every shipping carton?
By standardizing technical requirements, setting clear pre-production approval gates, and partnering with an audited rg cable factory, procurement managers eliminate supplier risk, control lead times, and secure consistent high-performance RF coaxial cable assemblies.





